



Accurately determining the mesh size of a filter is a fundamental requirement for maintaining industrial filtration standards and ensuring particle separation efficiency. In technical terms, "mesh" refers to the number of openings per linear inch of the screen material. While it sounds simple, the precision of this measurement can be the difference between a perfectly functioning system and one plagued by downstream contamination or excessive pressure drops. Whether you are identifying a replacement part for a legacy machine or verifying the quality of a new shipment, knowing how to measure mesh size with precision is a core competency for any engineer or technician.
In high-precision manufacturing sectors-such as semiconductor fabrication, aerospace fuel systems, and pharmaceutical purification-"close enough" is never sufficient. A deviation of even a few microns in the aperture size can compromise the integrity of a batch or lead to catastrophic failure in sensitive hydraulic components. Measuring mesh size is not just about counting wires; it is an analytical process that involves understanding metallurgy, weave geometry, and the physical laws that govern fluid passage through a porous medium. This guide provides a 3000-word deep dive into the methodologies used to quantify mesh size, ranging from manual field techniques to the cutting-edge automated optical analysis used in smart factories.
The Fundamentals of Mesh Anatomy and Geometry
The "Linear Inch" and Historical Context
The concept of "Mesh" is rooted in the history of the wire weaving industry. By definition, mesh count is the number of wires (and consequently the number of openings) in one linear inch ($25.4$ mm). This measurement is taken from the center of one wire to the center of another wire one inch away. Historically, this allowed for a standardized way to trade and specify sieves. However, as filtration requirements moved into the sub-100 micron range, the limitations of this "count-based" system became apparent. It does not account for the thickness of the wires, which led to the development of the "Micron Rating" system to provide a more absolute measurement of the filtration gap.
Aperture: The Critical Gap
The Aperture ($w$) is the most critical dimension for filtration. It is the clear distance between the edges of two adjacent parallel wires. While the mesh count tells you how many "units" are in an inch, the aperture tells you the maximum size of a particle that can physically pass through the screen. Measuring the aperture requires higher precision than counting the mesh, as localized variations in the weaving process (such as wire "shifting") can cause significant fluctuations in aperture size across a single roll of mesh, even if the overall mesh count remains correct.
Wire Diameter and Its Volumetric Impact
Wire Diameter ($d$) is the thickness of the metal strand before weaving. In the measurement process, the wire diameter is the "silent partner" of the mesh count. Two screens with a 100-mesh count can have vastly different properties if one uses a $0.030$ mm wire and the other uses a $0.050$ mm wire. The thicker wire creates a smaller aperture and a more robust screen, but it also reduces the total "open area," which can lead to higher resistance to flow. Measuring wire diameter accurately requires a micrometer with a friction thimble to avoid compressing the metal during measurement.
The Concept of Pitch and Its Calculation
The Pitch ($p$) is the center-to-center distance between two adjacent wires. It is mathematically expressed as $p = w + d$. For technicians, measuring the pitch is often easier than measuring the aperture directly, especially in fine meshes. By measuring the total distance across 10 or 20 pitches and dividing by that number, you can derive an average pitch that smooths out minor manufacturing deviations. This average pitch is then used to verify the mesh count: $Mesh Count = 1 / p$ (when $p$ is in inches).
Advanced Weave Geometries and Measurement Nuances
Square Weave Measurement Dynamics
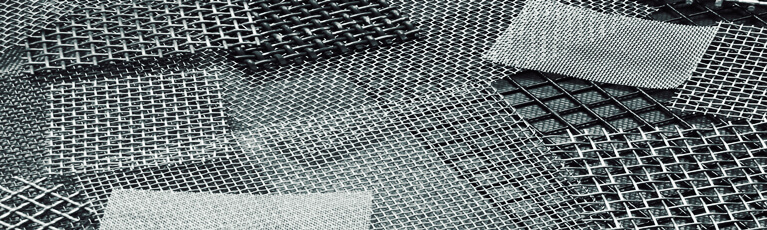
In a standard Square Weave (Plain or Twill), the wires are interlaced in a 1:1 or 2:2 ratio. Measurement is relatively straightforward because the openings are (theoretically) perfectly square. However, during the weaving process, tension in the "Warp" (lengthwise) and "Shute" (crosswise) directions may differ. This results in "Off-count" mesh, where a screen specified as 100-mesh might actually be $100 \times 98$. Accurate measurement requires taking samples in both orientations to ensure the filter performs uniformly across its surface.
Dutch Weaves: The Complexity of Overlap
Dutch Weaves (Plain Dutch, Twill Dutch, and Reverse Dutch) do not have square openings. Instead, the shute wires are driven tightly together, creating a "wedge-shaped" opening. You cannot measure these using a ruler. They are specified with two numbers, such as $24 \times 110$ mesh. The "24" refers to the warp count, and the "110" refers to the shute count. Measuring the "size" of a Dutch weave involves determining the Absolute Micron Rating, which is the diameter of the largest hard spherical particle that can pass through the complex, tortuous path of the overlapping wires.
Five-Heddle Weave and Pattern Repeat
The Five-Heddle weave is a specialized industrial pattern where each shute wire passes over four warp wires and under one. This creates a smooth surface on one side, which is excellent for filter cake removal. Measuring this weave requires the technician to identify the "Pattern Repeat." Counting only a few wires can lead to a significant error because the pattern is not symmetrical over short distances. One must measure across at least five pitches to capture a full cycle of the weave and determine the true mesh count.
Knitted Mesh: Density vs. Aperture
Knitted wire mesh is produced by interlinking loops of wire, similar to a sweater. It has no "mesh count" in the traditional sense. Measurement of knitted mesh is based on loops per linear inch and the density of the mesh (the percentage of volume occupied by metal). Measuring knitted mesh requires a "Yield Test," where a specific volume of the mesh is weighed. For demisters and acoustic dampening, the surface area per unit volume is the key metric, which is calculated based on the wire diameter and the loop geometry.


Manual Measurement: Field Tools and Techniques
The Linen Tester and Its Professional Use
A linen tester is a specialized, folding magnifying glass with a calibrated scale at its base. It is the most common tool for field verification of mesh sizes between 20 and 150. To use it correctly, the base must be placed flat against the mesh to ensure the focal length is consistent. The technician counts the wires within the 1-inch or 1/2-inch scale. To avoid "Parallax Error," the eye must be positioned directly over the center of the lens. This tool is indispensable for receiving-dock inspections where a quick verification of the mesh count is required.
The Mesh Gauge (Optical Interference Method)
A mesh gauge is a transparent plate with a set of diverging lines. When placed on a mesh, it creates a Moiré pattern. The convergence point of the pattern points to a number on the scale, indicating the mesh count. This is a non-contact, rapid-assessment tool. However, its accuracy is limited to standard square weaves. It cannot be used for Dutch weaves or multi-layer sintered mesh. It is a "go/no-go" tool used primarily to ensure that a 60-mesh screen hasn't been accidentally replaced by a 50-mesh screen during a maintenance shift.
Micrometers and Calipers: Precision Hardware
Digital micrometers are the primary instruments for measuring wire diameter ($d$), while digital calipers are used for larger apertures ($w$). In a professional setting, these tools must be calibrated against gauge blocks. A specific technique called "The Ten-Wire Measure" is used for fine mesh: measure the distance across ten wires, subtract the total thickness of ten wires (measured by a micrometer), and divide the result by ten to find the average aperture. This reduces the error inherent in trying to measure a single tiny gap with bulky caliper tips.
The "Feel" of the Weave: Qualitative Indicators
Experienced technicians often use qualitative methods to supplement their measurements. The "rigidity" of the mesh and the "light transmission" are indicators of the open area. While not a substitute for quantitative data, if a measured 100-mesh screen feels significantly more flexible than a known standard, it suggests the wire diameter is thinner than specified. This qualitative assessment often triggers a more detailed laboratory analysis to verify if the mesh meets the required tensile strength standards.
Advanced Laboratory Analysis and Porometry
Digital Microscopic Imaging (DMI)
Digital microscopy allows for magnification levels up to $1000x$, where individual wire surface defects can be seen. Integrated software can automatically detect the edges of the wires and calculate the area of every opening in the field of view. This provides a "Distribution Map" of the apertures. In high-stakes filtration, it is not enough to know the average mesh size; you must know the maximum aperture size, as a single oversized hole can allow a "contaminant bypass."
Optical Comparators and Shadowgraphy
An optical comparator projects a magnified shadow of the mesh onto a glass screen. The operator uses a digital readout (DRO) to move the stage from one wire edge to the next. This is a non-contact method, which is crucial for very fine or soft meshes (like Nylon or Copper) that might be deformed by the touch of a micrometer. Shadowgraphy is the preferred method for certifying mesh according to ASTM E11 standards, as it eliminates human error in aligning caliper tips with microscopic wire edges.
Bubble Point Testing (Capillary Flow Porometry)
For complex filters like sintered fiber felt or multi-layer Dutch weaves, the physical wires cannot be counted. Instead, the Bubble Point Test is used. The filter is saturated with a liquid of known surface tension, and air pressure is gradually increased. The pressure at which the first bubble appears (the "First Bubble Point") is used to calculate the largest pore size using the Washburn Equation: $D = 4\gamma \cos\theta / P$. This provides an "Absolute" measurement of the filter's performance that counting wires simply cannot provide.
Scanning Electron Microscopy (SEM) for Sub-Micron Mesh
In the semiconductor and biotech industries, mesh sizes can reach the sub-micron level. For these applications, SEM is required to verify the mesh structure. SEM provides incredible depth of field, allowing engineers to inspect the "internal" layers of a sintered mesh stack. This is used to ensure that the "Diffusion Bonding" process during sintering hasn't closed off too many pores or caused the fine wires to melt and merge, which would drastically alter the mesh's permeability.
Identifying the correct mesh count is only as reliable as the instrument in your hand. Whether you are performing a quick field check with a manual loupe or a certified laboratory audit using high-resolution vision systems, selecting the right hardware prevents significant margins of error. For a detailed comparison of the latest digital micrometers, optical comparators, and microscopic inspection systems, see our professional review:
[Top 5 Tools for Measuring Filter Mesh Size: A Professional Review]


Mathematical Conversions and Flow Dynamics
The Mesh-to-Micron Mathematical Conversion
While a "Conversion Table" is useful, engineers should know the underlying math. The conversion depends entirely on the wire diameter (d).
The formula to find the aperture (w) in microns from mesh count (M) and wire diameter (d in mm) is: w (microns) = [(25.4 / M) - d] * 1000
This formula highlights why two "100-mesh" screens can have different micron ratings. If one has a 0.10 mm wire and the other has a 0.12 mm wire, their micron ratings will be 154 microns and 134 microns respectively-a 13% difference in filtration performance.
Calculating the Percentage of Open Area
The Open Area (OA) is the ratio of the area of the openings to the total area of the mesh. It is calculated as: OA% = [w^2 / (w + d)^2] * 100
This metric is vital for calculating the "Pressure Drop" (Delta P) across the filter. A lower open area increases the velocity of the fluid through the pores, which can lead to "Particle Shearing" or premature clogging. Custom-made filters are often designed by selecting a mesh count and wire diameter combination that yields a specific OA% to meet flow requirements.
Effective Filtration Area (EFA)
When measuring a filter, the EFA is the actual surface area through which the fluid passes. This is not just the area of the mesh; in a pleated filter, the EFA is much larger. Measuring the mesh size of a pleated filter requires "unfolding" a sample to determine the pleat count and depth. The total EFA is then used in conjunction with the mesh size to determine the filter's "Dirt Holding Capacity." A finer mesh requires a larger EFA to maintain a reasonable service life between cleanings.
Permeability and the Darcy's Law Relationship
Mesh size measurement data is used as an input for Darcy's Law to predict fluid flow: Q = (k * A * Delta P) / (u * L). The permeability (k) is a function of the mesh aperture and the open area. By accurately measuring the mesh dimensions, engineers can model the entire filtration system's behavior in software like CFD (Computational Fluid Dynamics) before the filter is even manufactured. This demonstrates how a simple "count" of wires scales up into complex system-wide engineering.
Understanding the math is only the first step. For a complete set of industry-standard tables and advanced formulas for varying wire diameters, explore our comprehensive guide:
[Mesh to Micron: The Ultimate Conversion Guide]
Industrial Standards and Compliance (ASTM & ISO)
ASTM E11: The Standard for Test Sieves
ASTM E11 is the most widely recognized standard for wire cloth used in testing. It classifies sieves into three categories: Compliance, Inspection, and Calibration. Measuring a mesh for ASTM compliance involves not just finding the average aperture but also ensuring that no single aperture exceeds the "Maximum Individual Opening" limit. For example, a standard 100-mesh sieve has an average aperture of $150 \mu m$, but the standard allows for an individual opening up to $174 \mu m$ in a "Compliance" grade sieve.
ISO 9044: Industrial Wire Cloth Standards
While ASTM is common in the US, ISO 9044 is the international standard for industrial wire cloth. It defines the "allowable deviations" for aperture and wire diameter. Measuring for ISO compliance requires a statistical approach-taking measurements at at least 10 different locations on a roll. The standard also covers "Weaving Defects," such as broken wires or "overshot" shute wires, which must be identified and marked during the measurement and inspection process.
Pharmaceutical and Food Grade Certification (FDA)
When measuring mesh for the food or pharmaceutical industry, the focus shifts to "Surface Finish" and "Cleanability." In addition to the mesh size, the Ra value (surface roughness) must be measured. FDA-compliant mesh is often electro-polished after weaving. Measuring the mesh count of electro-polished cloth is more difficult because the chemical process slightly thins the wires, which in turn slightly increases the aperture. A 100-mesh screen might become a "102-mesh" equivalent after aggressive polishing.
Aerospace and Military (MIL-SPEC) Standards
In aerospace, mesh filters (like those in hydraulic lines) are governed by strict MIL-SPEC or NAS standards. These require "Traceability" to the original melt of the wire. Measurement in this sector often involves "Non-Destructive Testing" (NDT). The mesh size is verified through a combination of optical measurement and a "Flow Test," where the pressure drop across the filter is measured using a standardized fluid at a specific temperature. If the flow resistance is too high, the mesh is rejected, even if the count is correct.
Navigating the specific tolerances allowed by global engineering bodies is essential for quality assurance. For a detailed breakdown of certification protocols, see our specialized article:
[ASTM and ISO Standards for Mesh Specification]
Comparison of Global Mesh Standards
| Standard | Primary Application | Focus of Measurement | Typical Tolerance |
| ASTM E11 | Laboratory Testing | Individual Aperture Max | Very Strict |
| ISO 9044 | Industrial Fabrication | Average Aperture/Wire | Moderate |
| DIN 4189 | European General Use | Weave Uniformity | Moderate |
| NAS 1638 | Aerospace Hydraulics | Fluid Cleanliness/Micron | Extremely Strict |

The Impact of Environmental Factors on Measurement
Thermal Expansion and High-Temp Measurement
Mesh screens used in furnaces or hot gas filtration will expand during operation. If you measure a mesh at 20°C, its aperture will be significantly larger at 800°C. This is due to the Coefficient of Thermal Expansion (CTE). For critical high-temp applications, engineers must use the "Calculated Operating Aperture." For example, Stainless Steel 310 will expand about 1.5% at high temperatures, which might turn a 100 micron filter into a 101.5 micron filter. This must be accounted for during the measurement and specification phase.
Mechanical Tension and "Mesh Elongation"
When mesh is installed in a frame, it is tensioned. This tension slightly stretches the wires, which increases the aperture size and decreases the mesh count. In screen-printing or vibratory sieving, "Tension Meters" are used to measure the force applied (usually in Newtons). A measurement of the mesh count must be taken after tensioning to ensure the openings have not distorted into rectangles. If the tension is uneven, the mesh will have different "counts" in the center versus the edges.
Corrosion and Wire Thinning
In corrosive environments, the wire diameter (d) will decrease over time as the metal is eaten away. This "Thinning" increases the aperture size (w) and the open area, but it also significantly weakens the mesh. Measuring a "used" filter often reveals that it is no longer performing at its original micron rating. Regular "Maintenance Measurements" are required to determine when the wire has thinned to a critical point (usually 10-20% loss of diameter) where the risk of the mesh snapping becomes too high.
Pressure-Induced Deformation (Blinding and Bursting)
Under high fluid pressure, a fine mesh can "bow" or "distend." This mechanical deformation changes the shape of the openings from squares to diamonds, a phenomenon known as "Mesh Distort." Measurement of this effect is done using "Pressure-Volume" curves. If the mesh is not supported by a rigid core, the "Effective Mesh Size" changes as the pressure increases. This is why high-pressure filters are often sintered-to lock the wires in place and prevent any pressure-induced changes in aperture size.
Automated Measurement and Industry 4.0
Machine Vision Systems on Weaving Looms
In modern "Smart Factories," mesh is measured as it is being woven. High-speed cameras mounted on the loom scan the mesh in real-time. If the system detects that the shute wire has shifted by even a few microns, it automatically adjusts the loom's tension. This creates a "Digital Twin" of the entire roll of mesh, documenting the exact mesh size and any localized deviations. This level of automated measurement ensures a level of quality that manual counting can never achieve.
AI and Pattern Recognition for Defect Detection
Artificial Intelligence is now used to analyze the images captured by optical inspectors. AI algorithms can distinguish between a "harmless" cosmetic defect (like a slight wire discoloration) and a "critical" dimensional defect (like a loose wire). By training on thousands of images, the AI can measure the "Uniformity Index" of the mesh. This index tells the engineer how consistent the aperture size is across the entire surface, which is a key predictor of the filter's performance in high-purity applications.
IoT-Enabled Filter Monitoring
The future of mesh measurement is in the "In-Situ" monitoring of filters via the Internet of Things (IoT). Sensors measure the pressure drop and flow rate in real-time and send this data to the cloud. By analyzing the "Flow Signature," software can infer if the mesh apertures are clogging (blinding) or if they have enlarged due to corrosion. This "Virtual Measurement" allows companies to replace filters based on actual performance data rather than a fixed calendar schedule, optimizing both safety and cost.
Digital Certification and Blockchain Traceability
As the accuracy of measurement increases, so does the need for secure documentation. Many high-end mesh manufacturers are now moving toward "Digital Certificates" stored on a blockchain. The exact measurements taken in the lab-aperture, wire diameter, tensile strength-are linked to a QR code on the roll of mesh. This ensures that the measurement data cannot be tampered with and provides the end-user with absolute confidence that the filter they are installing meets every technical specification.
Common Measurement Errors and Solutions
| Common Error | Technical Impact | Corrective Action |
| Excluding Wire Diameter | Overestimates opening size | Always use $w = p - d$ formula |
| Counting in one direction only | Misses rectangular openings | Always measure Warp and Shute directions |
| Using damaged mesh samples | Leads to inconsistent data | Measure multiple "healthy" areas and average |
| Parallax Error with Rulers | Inaccurate linear count | Use a digital caliper or optical loupe |
| Ignoring Tension Effects | Aperture distortion | Measure mesh after installation/tensioning |
| Relying on Nominal Ratings | Risk of contaminant bypass | Perform Bubble Point test for Absolute rating |
Conclusion
Measuring the mesh size of a filter is a technical skill that blends physical observation with mathematical validation. As we have demonstrated, a simple count of wires per inch is only the starting point. To achieve professional-grade accuracy, one must meticulously measure the wire diameter, calculate the pitch, and account for the specific weave style. Whether you are in the field using a simple linen tester or in a laboratory using automated optical inspection, the goal remains the same: ensuring the filtration aperture matches the requirements of the process.
In the final analysis, the precision of your mesh measurement directly impacts the efficiency, safety, and cost-effectiveness of your industrial operations. By avoiding common pitfalls like parallax error and ignoring off-count weaves, and by utilizing the correct formulas for open area and aperture, you can maintain the high standards required in modern engineering. Accurate measurement is the foundation of quality control, allowing for the seamless replacement of parts and the optimization of filtration systems across all industrial sectors. In an era where manufacturing precision continues to push the boundaries of the microscopic, mastering the science of mesh measurement is more critical than ever.